Aluminum Laser Cutting & CNC Pipe Bending Services
Hongsinn-752
Need reliable OEM laser cutting and CNC pipe bending services? Our advanced technology delivers exceptional accuracy and efficiency for all your fabrication needs. Reach out now to discuss your project!
Delivery
FOB
minimum order
1 piece
Supply Ability
5000piece / Week
Country of Origin
Shenzhen
Stock Time
7~15Day
Quantity:
US $0.59 - US $10.68 / piece
Aluminum Laser Cutting & CNC Pipe Bending Services
For engineers, product designers, and purchasing managers, finding a full-service manufacturing partner can streamline production, reduce costs, and ensure superior quality. Three key services that form the backbone of modern manufacturing are aluminum laser cutting services, OEM laser cutting services, and CNC tube bending services.

Hongsinn offers a full range of tube bending capabilities and services. These services include:
• Mandrel tube bending
• Rotary stretch tube bending
• Coil tube bending
• Compression bending
Mandrel Tube Bending
Mandrel tube bending (also known as mandrel bending) is a method similar to rotary stretch bending, but it fully preserves the tube profile throughout the entire bend. This process uses an internal support called a mandrel to maintain the tube's structure during the bending process, ensuring minimal unwanted deformation.
A mandrel tube bending machine is equipped with a long bed and a mandrel rod, which is fixed at the bender's tangent point. The tube slides over the mandrel, which is clamped and bent while the mandrel remains stationary. Mandrel tube bending is particularly suitable for tubes with thin walls, large diameters, and tight bend radii, where collapse is more common.
Rotary Stretch Tube Bending
Rotary stretch tube bending is one of the most popular methods currently used. This method uses a clamping die, a radius (or bend) die, and a pressure die to maintain the tube's shape throughout the bending process. The tube is clamped to the bending die and"pulled"around the other dies hydraulically or electrically, resulting in a highly precise and repeatable bend.
The rotary stretch tube bending process can be manual, semi-manual, or CNC-controlled. Computer-guided rotary stretch bending offers unparalleled precision, making it particularly suitable for high-volume applications. However, setup times can be lengthy, and each unique bend requires specialized tooling.
|
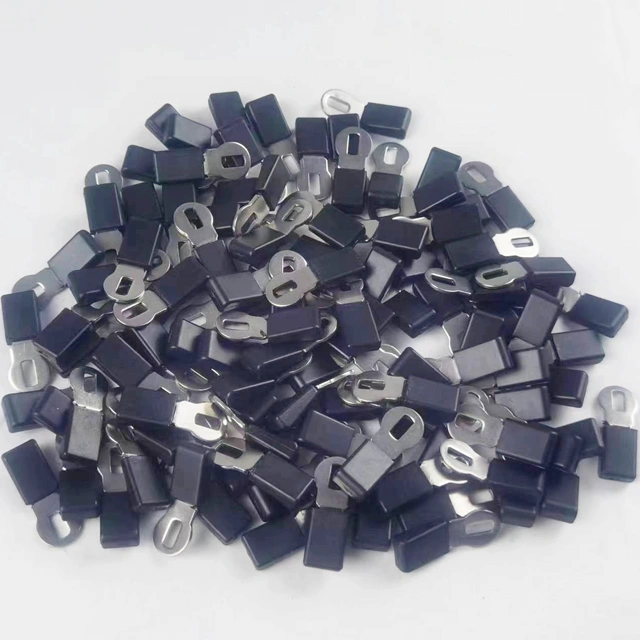
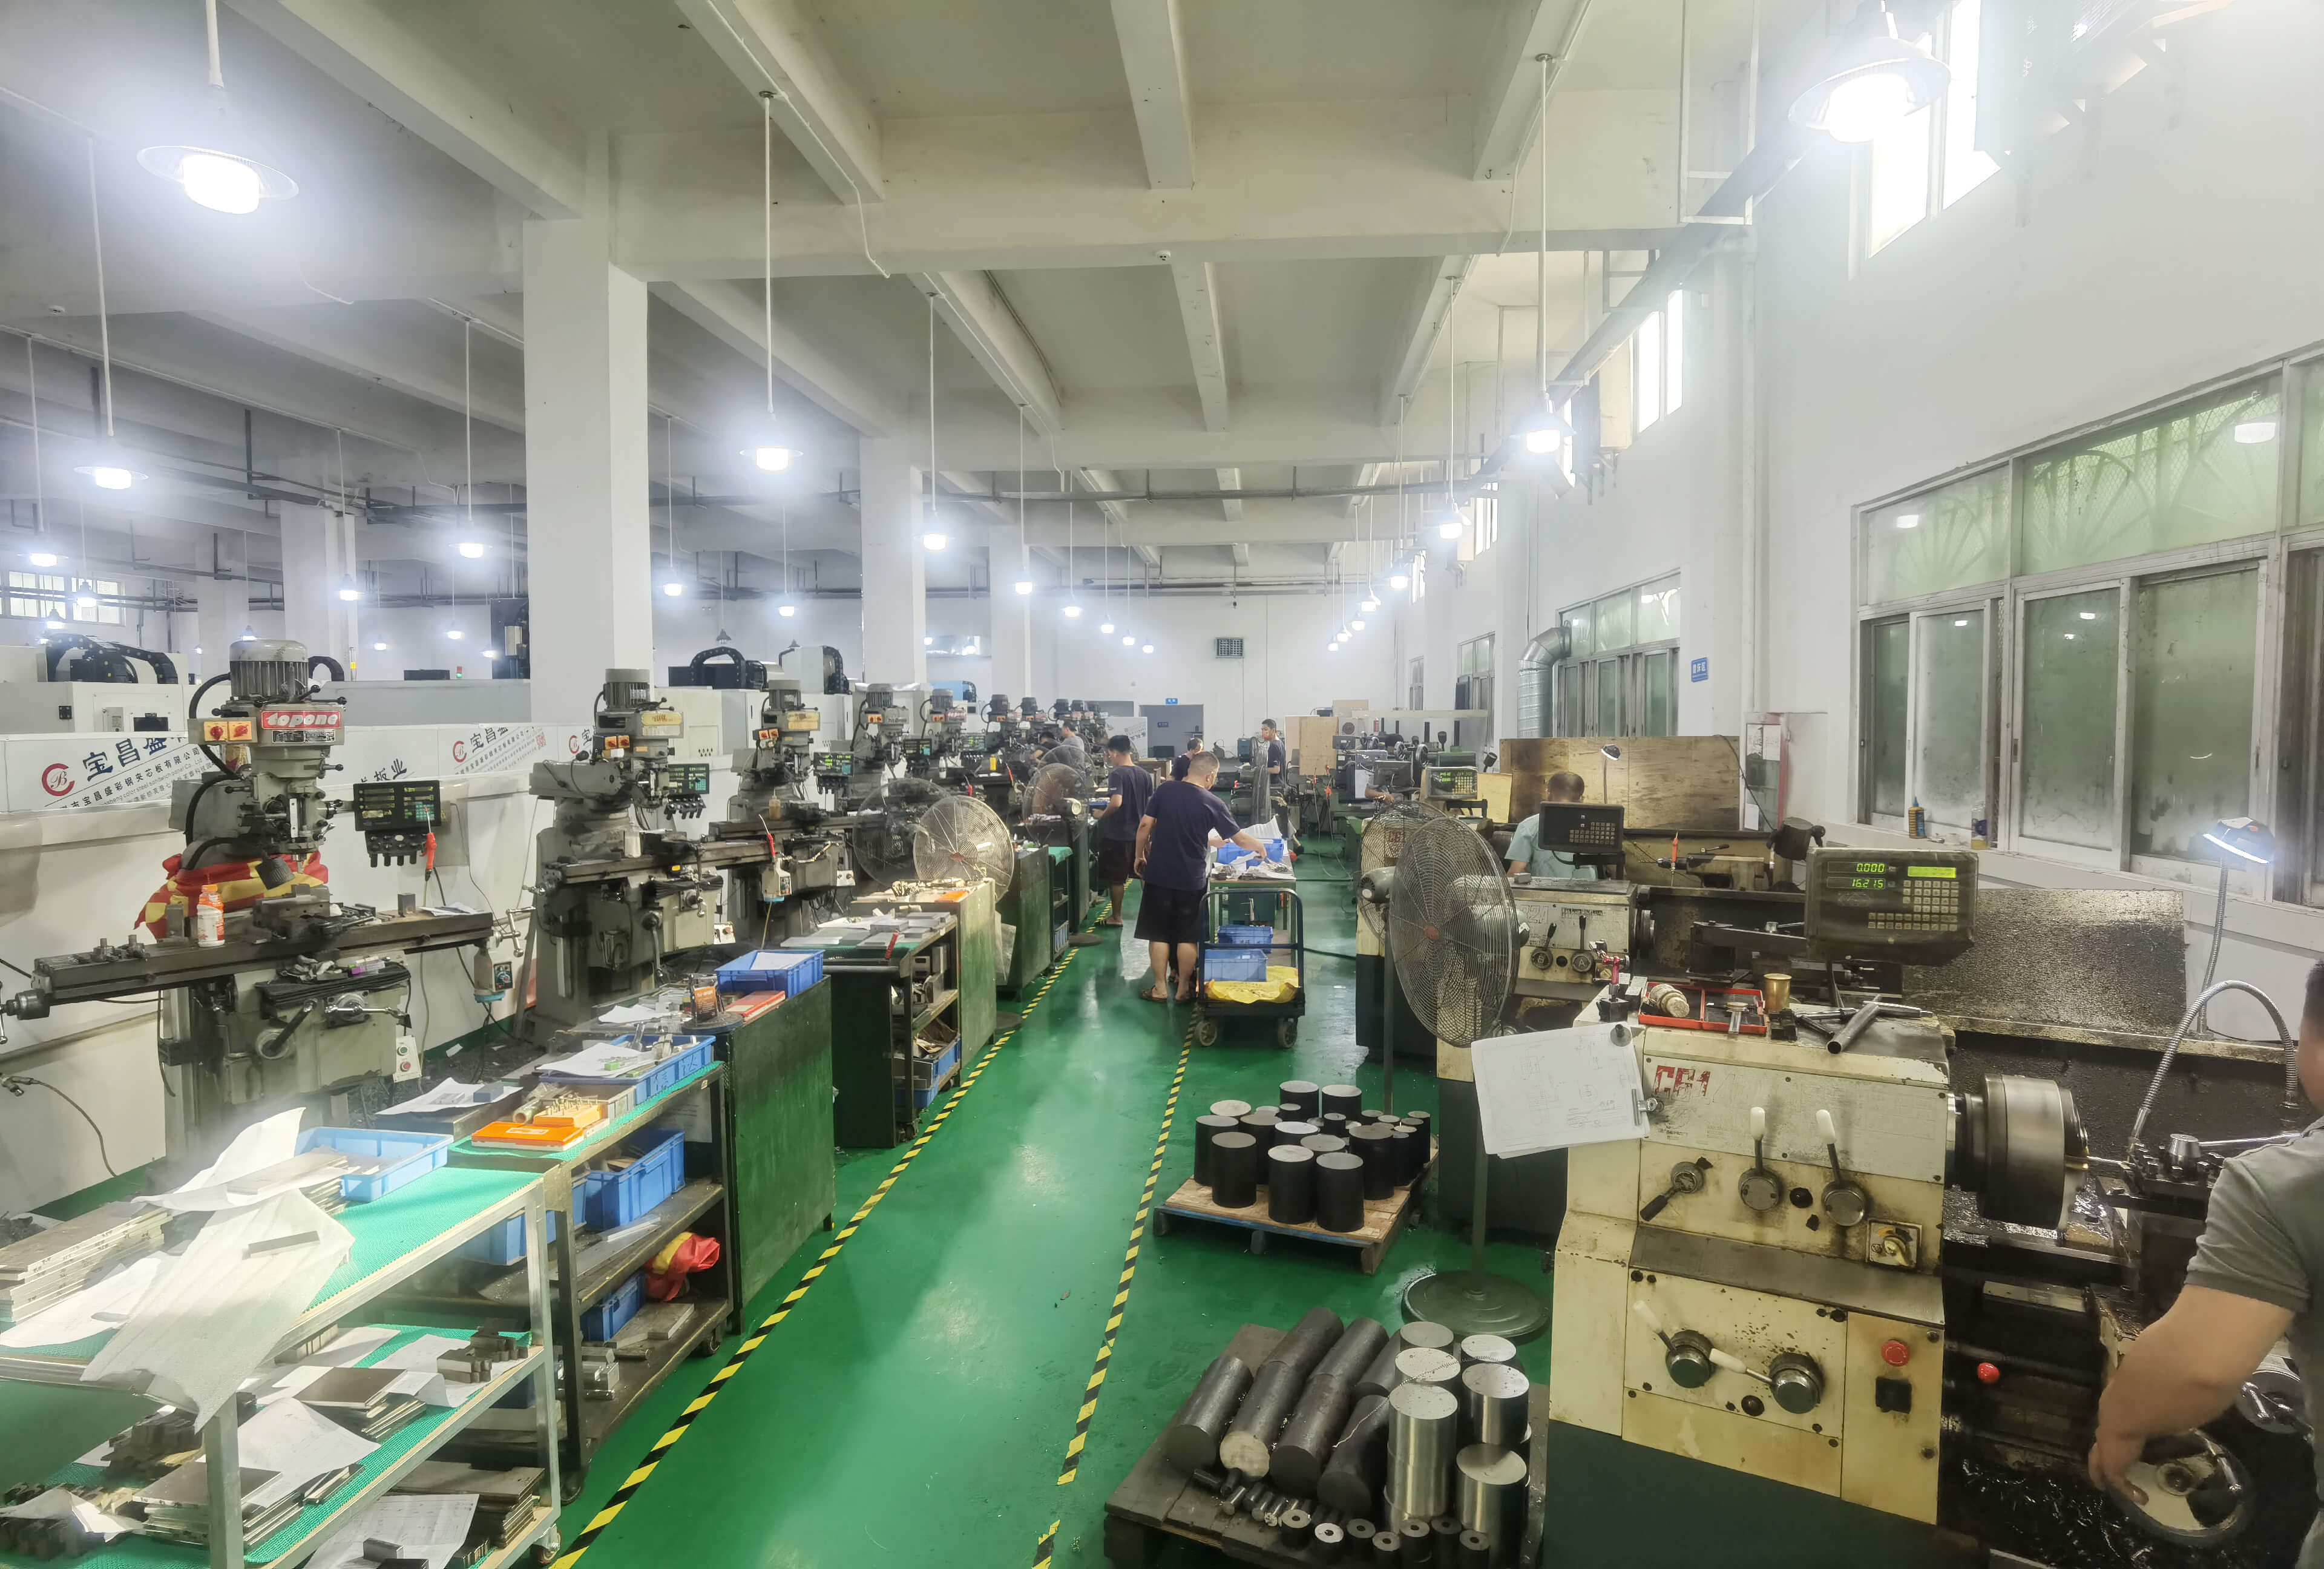
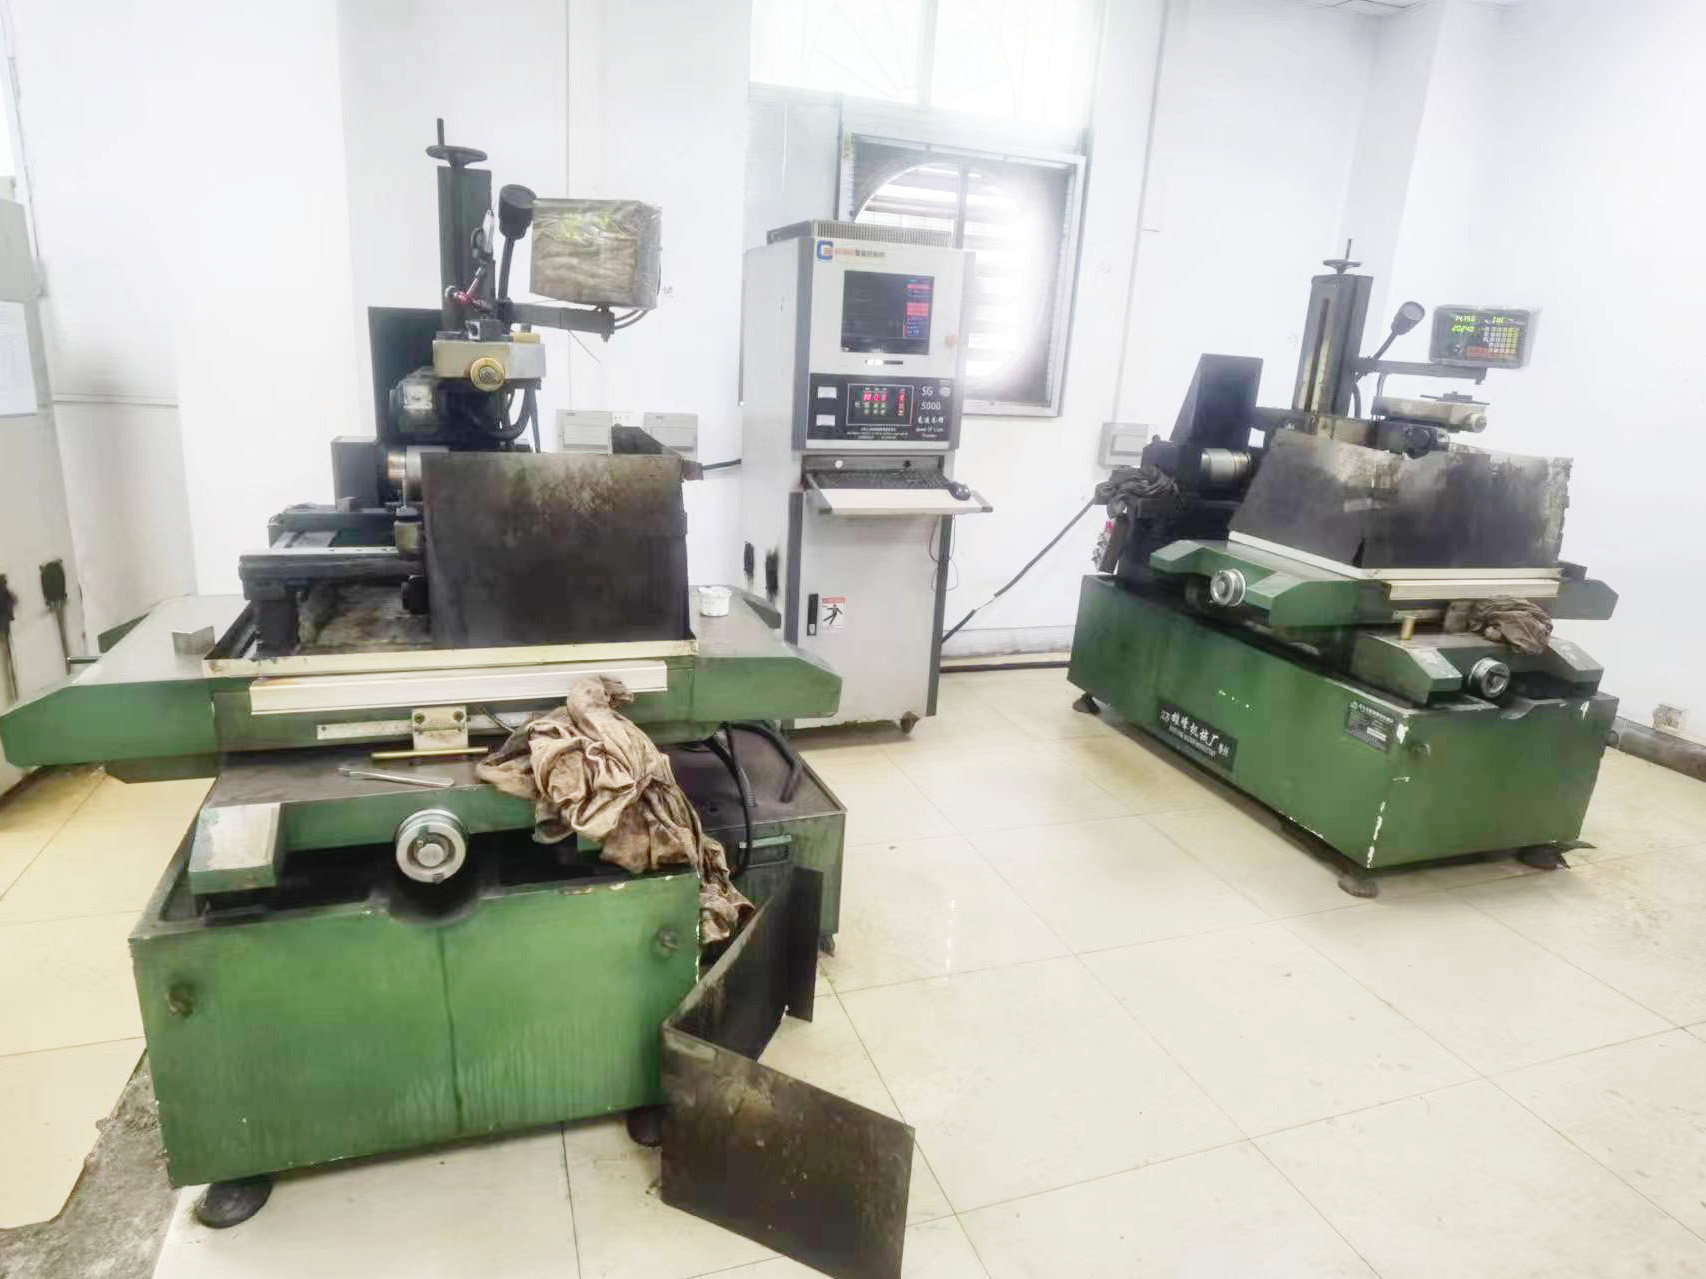
Sheet Metal Fabrication can be made of stainless steel, carbon steel. aluminum, galvanized steel. etc.
Pls Send us your drawing or sketch, we can make sample for your testing quality before mass production.
We also make other sheet metal fabrication products. For example, laser cutting parts, bending parts, welding parts,
Most Popular is electric box enclosure, metal battery cabinet welcome in Australia, USA, please Contact Us for more details
We also make other sheet metal fabrication products. For example, laser cutting parts, bending parts, welding parts,
Most Popular is electric box enclosure, metal battery cabinet welcome in Australia, USA, please Contact Us for more details
Roller Tube Bending
Roller tube bending (also known as roll bending) is a process that uses three dies (or rollers) to lock the tube. During this process, a piston applies pressure to the tube, and the operator"rolls"the tube through the machine, creating a gradual bend (also known as an arc). The tube returns to its original position in the dies, the piston is lowered further, and the process is repeated until the desired profile is achieved.
This method is typically manually driven, but can also be motorized to provide additional power input. Roller tube bending offers variable bends and angles without the need for additional tools, making it suitable for large and gradual bends. However, its accuracy and repeatability are relatively limited.
Compression Bending
Compression bending is a process in which a tube or pipe is clamped in place and force is applied directly to create a bend. This method is primarily used for single-bend applications. Compression bending does not utilize internal supports, and therefore typically results in an oval cross-section, which can increase the risk of bend breakage.
In this process, bends are typically limited to angles of 120 degrees or less to ensure structural integrity and reduce the likelihood of breakage.